
Buyers usually ask a precision machining factory one question first: how long will it take? The useful version of that question is quieter and more specific, which steps must finish before the part can leave, which of those steps cannot be overlapped, and what has to be true on which day for the ship date to hold. A factory lead time is not a single duration a supplier carries in its head; it is the sum of a chain of dependencies, each with its own day cost, and the buyer who can see the chain can plan around it, compress it, and verify it while there is still time to act. This guide is built around that chain: how to work a schedule backward from your own deadline, how to recognize the step that owns the window, and how to manage a supplier on gates instead of on a final date alone.
Why should you plan a machining order backward from the ship date?
Forward planning starts from today and asks when the part might arrive; backward planning starts from the date the part must be usable and works out what has to happen before then. The difference matters because the two methods treat the same order differently. Forward planning tends to accept whatever the supplier quotes and then adds anxiety as the date approaches. Backward planning exposes the real constraint immediately: if the part must be on your line on a specific day, then the factory's ship date is fixed by the freight mode, the freight pickup is fixed by the factory's inspection gate, and the inspection gate is fixed by everything upstream of it. The calendar builds itself, and the only question left is whether the supplier's honest estimate fits inside it.
Working backward also changes what you ask for at quoting. Instead of "how long will my part take," you ask "here is the ship date the schedule requires, which steps would have to move for that date to be reachable, and which of them can move?" A factory that answers with a route and its constraints is engaging with your deadline as a planning problem; one that answers with a fixed duration is quoting its comfort zone. On overseas orders the backward method is not optional polish, because the freight leg alone can consume a week or more and the receiving leg adds days that forward planning almost always forgets.
Which dependencies decide the realistic window before you ask for a date?
Every machined order runs on a handful of dependencies, and naming them before asking for a date is what separates a plan from a guess. The first dependency is the released drawing: machining cannot start, and often material cannot be bought, until the geometry is frozen at a revision you and the factory agree on. The second is the material lot — the grade, the form, and the certificate have to be real and on the floor, and a special-order alloy injects a procurement window that no machining estimate can shrink. The third is the process route itself, including any step that has to be performed off-site, because a coating, a heat treatment, or a grinding pass with its own queue cannot be overlapped with anything else on the route.
The last dependency is the one buyers underestimate most: the inspection and documentation gate. A part is not ready when it comes off the machine; it is ready when the critical features have been measured, the report has been written against the released revision, and the paperwork has cleared whatever your receiving process demands. A factory that quotes a date without naming these dependencies is quoting a hope, because any of them can consume days that the estimate did not count. The practical move is to list the dependencies in writing at the quoting stage, so the schedule is an argument about a chain rather than an argument about a number.
How do you build a week-by-week calendar when the part carries finishing steps?
Once the dependency list exists, the calendar is a matter of stacking the steps in the order they must run and letting each one's day cost land where it belongs. Consider a housing that needs hard anodizing after milling: the machining route might occupy the first working week, the anodize batch runs on a vendor's cycle that starts on a particular weekday, and the post-coat inspection adds another block after the parts return. The calendar is not the machining estimate plus the anodize estimate; it is a sequence where the anodize window anchors the middle and everything else arranges itself around it. Sketching this on a simple table of weeks, with each step occupying its own row, makes the shape of the order visible in minutes.
The same exercise exposes where a schedule can actually be shortened. If the finishing step is the bottleneck, nothing you do to the milling route shortens the order; the lever is the finish itself — a different coating class, a shorter batch cycle, or an in-house process if one exists. If the material lot is the bottleneck, the lever is stock. If the machining route is the bottleneck, the lever is the geometry or the tooling plan. Building the calendar first, then asking where the days are thickest, is the difference between compressing a schedule and hoping it compresses itself. A factory that shows you its week-by-week stacking is inviting that conversation; one that guards its estimate as a single number is not.
What makes a quoted date slip, and which slips are actually your own doing?
The slips that hurt most are the ones that could have been seen. A quoted date moves for reasons that cluster into three groups: things the factory should have known when it quoted, things the buyer changes after the order, and things nobody controls. The first group includes an under-estimated route, a machine that was already over-booked, or a material the factory assumed would be in stock. The second group is the buyer's own territory: a revision sent after order release, a finish added after the quote, a document that arrives late and blocks shipment, or an approval that sits unsigned for days while the factory waits. The third group — weather on the freight leg, a customs hold, a holiday neither side planned around — is where the buffer belongs.
The discipline that cuts the middle group is to treat every post-order input as a schedule event. A revision is not an email; it is a restart of the steps it touches. An added finish is not a line item; it is a new dependency with its own queue. An unsigned approval is not a formality; it is the inspection gate waiting on you. When a buyer audits why a date slipped, the honest breakdown usually shows the factory's share and the buyer's share sitting side by side, and the buyer who tracks their own inputs on the same calendar as the factory's outputs is the buyer whose next order runs on a schedule instead of on hope.
How do approvals and drawing versions act on the schedule?
Approvals sit inside the schedule at two points that buyers rarely count. The first is before the order: the time your own team takes to review the factory's process notes, confirm the material callout, and sign the purchase order is real time, and every day it takes is a day the factory cannot spend ordering stock or booking the machine. The second approval point is the first-article review, where the factory's measured report meets your quality expectation; if the report sits in an inbox for days, the parts sit with it, because most factories will not ship the balance of an order until the sample gate is closed. Both approval points are buyer-owned dependencies, and both are invisible in the factory's quoted estimate, which assumes they resolve promptly.
Drawing versions act on the schedule with more force than most buyers assume because they invalidate work that already happened. A change that alters the envelope can make purchased material scrap before it is cut; a change that moves a feature can make a finished fixture useless; a change to a critical dimension can invalidate the inspection plan and the first-article report already produced. The version discipline that protects the schedule is the same one that protects quality: one released revision in the purchase order, all changes routed through a formal notice that restates the ship date, and no verbal change ever treated as an instruction. A factory that refuses to cut to an unreleased version is not being difficult; it is protecting the very schedule the buyer is asking about.
How should quantity and repeats change the way you book time?
Quantity changes the schedule through the steps that repeat, not through the steps that happen once. The route qualification, the inspection plan, and the first-article report are one-time work that a first order carries regardless of whether it buys ten parts or a thousand; the per-piece cutting time then scales with the quantity and is usually scheduled in production blocks rather than day by day. The practical effect is that a first order of one part and a first order of fifty parts share most of their schedule, because both pay for the same qualification and the fifty parts add cutting time measured in shifts rather than weeks. Buyers who multiply a per-part estimate by the quantity are double-counting the schedule; buyers who separate the one-time work from the running work are booking the calendar correctly.
Repeats change the picture because the one-time work disappears. The second order of the same released part reuses the program, the fixtures, the inspection method, and the approved first-article baseline, so its schedule is dominated by material and cutting time and is correspondingly shorter and more predictable. The planning habit that captures this value is to keep the first-order qualification package — the approved report, the fixture list, the material story — as a standing asset, and to tell the factory at the repeat-quote stage that the geometry is unchanged at the released revision. A supplier that knows a reorder is a reorder prices and schedules it as one; a supplier that must rediscover the geometry on every order charges the qualification twice and books the calendar twice.
What does a good supplier status report actually look like?
A useful status update names gates, not moods. A weekly report that says "material received and verified, machining scheduled to start Tuesday, next gate is the first-article measurement on Friday, no deviations" lets a buyer act on the information. A report that says "everything is on track" gives the buyer nothing, and a report that goes quiet for two weeks and then announces a delay has converted a manageable slip into an emergency. The discipline of named gates also forces the factory to know its own schedule, because a supplier cannot report a gate it has not planned. Buyers should ask for the gate format at the start of the order and accept nothing vaguer, because the cost of a precise weekly update is minutes and the value of early warning is measured in freight modes and line stoppages.
The buyer's side of the report loop matters just as much. A status report is only as good as the response it receives, and the response that protects the schedule is the one that resolves open items immediately — approving a sample, answering a drawing question, confirming a freight decision. Every item that waits on the buyer waits inside the schedule, and a supplier whose updates are answered within hours is a supplier whose schedule never stalls on the buyer's side. The reporting relationship that keeps an overseas order on time is a loop, not a one-way stream, and the buyers who run the loop tightly are the ones whose orders arrive when the calendar said they would.
How do you lock the plan in the order and keep it honest?
The schedule becomes enforceable when it is written into the commercial record at the level of gates, not just a final date. A purchase order that names the ship date, the released revision, the key milestone dates for the first article and the inspection release, and a duty to notify within a fixed number of days of any deviation gives the buyer a standing right to act on early warning. A purchase order that names only a final date gives the buyer nothing until the date has passed, at which point the only remedies are expensive ones. The gate-level order is also the tool that keeps both sides honest, because it converts the schedule from a shared hope into a shared checklist that either party can audit.
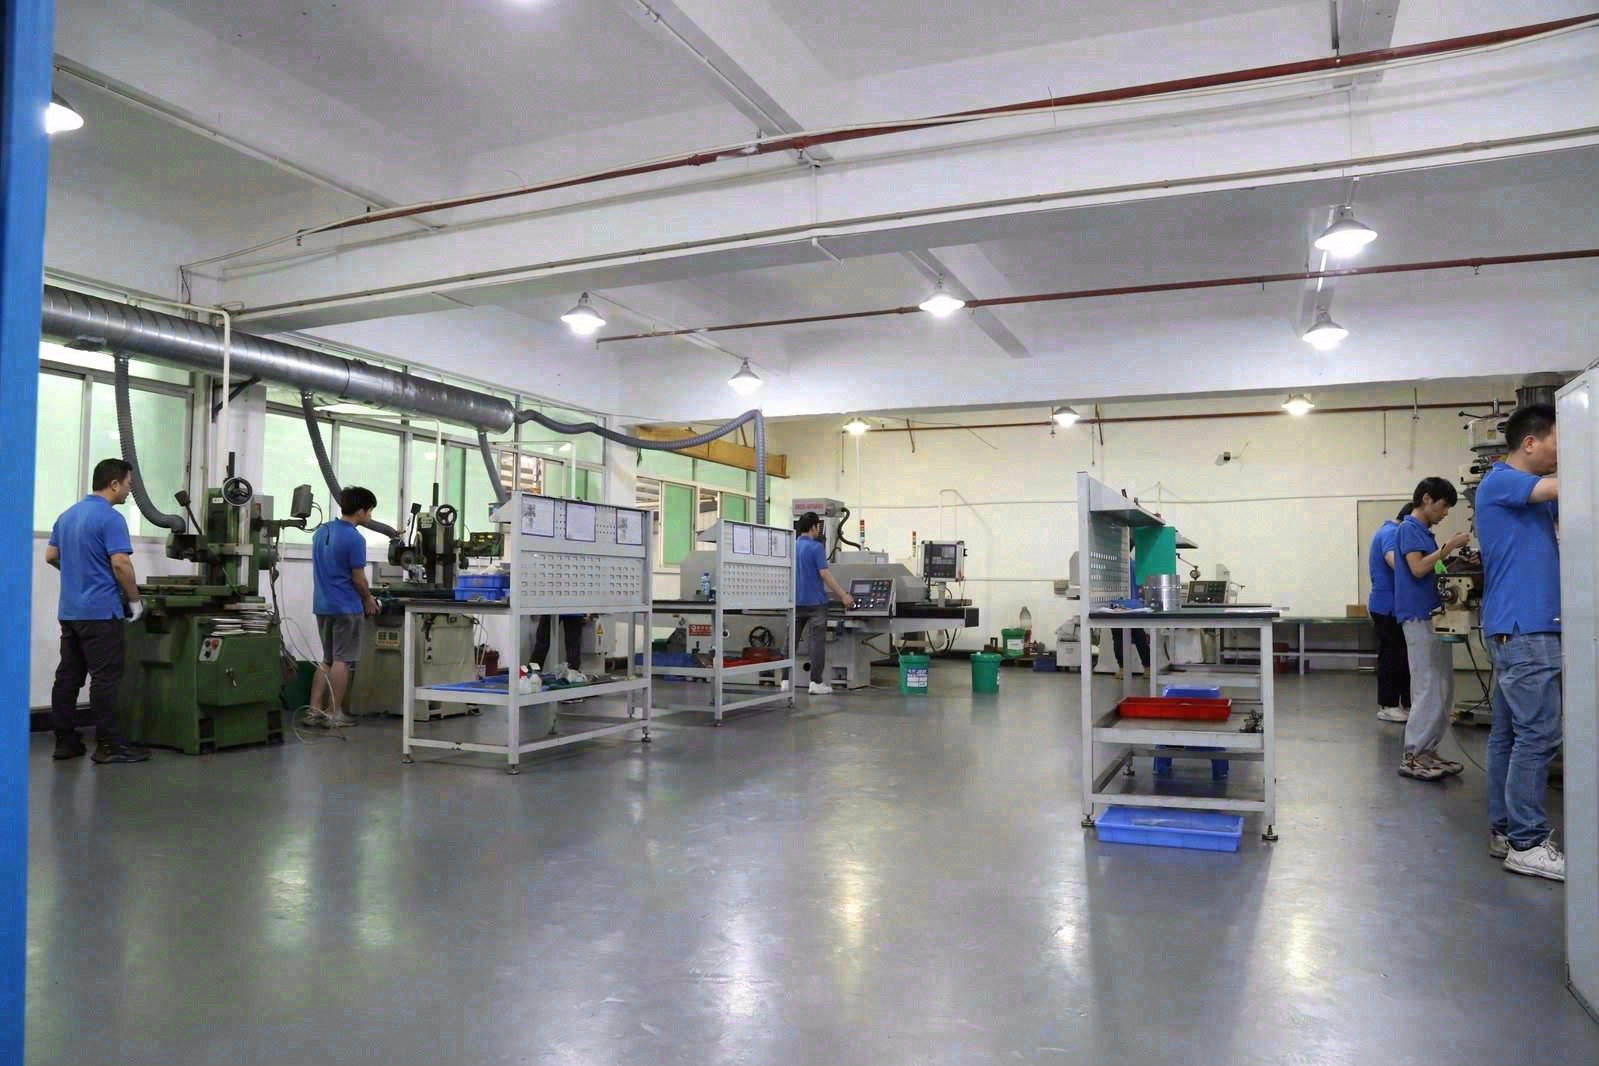
Keeping the plan honest after the order is a rhythm, not a one-time act. Review the gate dates weekly against actual progress, log every revision and every buyer-owned approval against the calendar, and when a date moves, record the reason and the new date in the same message rather than letting the change drift through email. The suppliers worth keeping welcome this rhythm, because it surfaces their own schedule problems while they are still small. The factory overview on this site shows the floor and the process flow a schedule is built against, the parts guide explains how geometry and tolerances translate into machining time, and the services page covers the finishing and secondary steps that often own the window. A schedule built on named dependencies, planned backward from the need date, and verified at gates is a schedule that ships; everything else is a forecast in need of a buffer.
Frequently Asked Questions
How many calendar days should I allow between an order and a part on my bench?
Take the factory's working-day estimate for the machining route, add the transit days of the freight mode you choose, add a customs and receiving margin, and only then convert the total back into calendar days. Working days and calendar days diverge quickly across a holiday or a weekend-heavy fortnight, so converting at the end rather than the start is where planning accuracy lives.
Which single dependency usually decides a precision part's delivery window?
Usually the step with the longest lead that nothing else can overlap: a coated surface, a heat-treated condition, or a certified bar that is not stocked locally. Once that step is named, the rest of the route schedules around it. A buyer who asks for the dependency list gets a schedule; one who asks only for a date gets an opinion.
What should a weekly progress update contain?
The current gate reached, the next gate scheduled, the material lot and certificate status, and any deviation with the date it was known. Updates that name gates give early warning while a slip can still be absorbed; updates that report vaguely after the promised date has passed are not updates at all.
How does a drawing revision really move the schedule?
A revision re-opens every step that already ran: the program, the tooling, the material bought to the old envelope, and the inspection plan built against the old datum structure. The honest factory states the new ship date the moment the revision is approved, not when the slip becomes unavoidable.
Why does my first order run slower than a reorder of the same part?
Because the first pass through a new geometry carries work that later orders reuse: proving the part machines as the drawing suggests, proving the inspection method on a real article, and locking fixtures and feeds. Once that baseline exists, a reorder reuses it and the calendar shrinks. The first-order premium is a qualification cost worth paying explicitly.
How much buffer is sensible on an overseas machining order?
Enough to absorb one realistic slip without breaking your downstream date. A practical pattern is one margin between the factory's ship date and the freight pickup, and a second between the estimated arrival and your hard need. Two small margins absorb a knock-on delay better than one large one at the end.
What belongs in the purchase order to make the schedule enforceable?
The agreed ship date, the released revision number, a short list of named gates with target dates, a duty to notify within a fixed number of days of any slip, and the inspection package as the condition for release. An order that names gates gives you the right to act on early warning; one that names only a final date gives you nothing until it is too late.
Want a ship date built from your need date instead of a stock answer?
Email the STEP or IGES model with your toleranced drawing to [email protected] or call +86 13126536955. You receive the dependency list for your part, the gate dates that follow from it, and a route that states which step owns the window.